A carton can look nearly perfect and still fail at the packing line. A label may sit a few millimeters off center, a seal may wrinkle, or the fill level may vary between shifts. Small differences matter. They affect product protection, shelf appeal, and customer confidence.
So, how to improve packaging consistency and accuracy? It starts with treating packaging as a controlled process, not a final visual check. Clear specifications, calibrated equipment, reliable materials, and practical operator training all help reduce variation. So do routine checks at key points, from incoming packaging supplies to finished cases. These measures are useful across many operations, but the right controls depend on the product, equipment, and production environment. A checklist alone cannot fix a poorly adjusted machine.
Quality expert W. Edwards Deming wrote, “It is not enough to do your best; you must know what to do, and then do your best.” His point applies to packaging: teams need defined standards and a way to verify them. The ten approaches below explore how to set those standards, monitor performance, and correct recurring errors. They focus on practical details, such as checking seal alignment and comparing measured fill weights with target ranges. Some improvements may seem obvious. Yet even experienced teams can overlook drift during a busy shift. Consistency takes attention—and occasional reconsideration of what the process is missing.
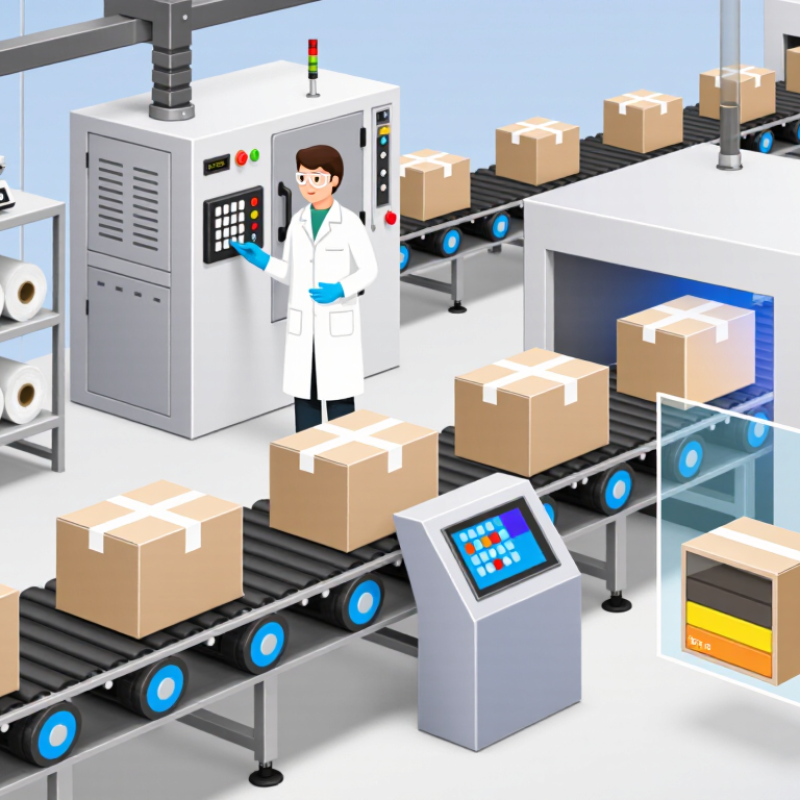
Packaging specifications turn expectations into checks that operators can repeat. Record each item’s dimensions, material, print position, closure type, and acceptable tolerances. For example, a carton might need to measure 200 by 150 millimeters, with a clearly defined allowance for variation. “Looks about right” is not a standard.
Make quality criteria measurable. Specify where a label should sit, how much text must remain readable, and what counts as a secure seal. Include reference photos showing acceptable and unacceptable examples. Keep approved samples near the packing line, where staff can compare them without leaving their station. Small details matter.
Standards should also describe how to inspect samples and record defects. A simple check might cover ten packs at the start of a shift, then repeat after a material change or machine adjustment. Track issues such as skewed labels, crushed corners, or inconsistent fill. Set clear actions for each failure, including who pauses production and who approves a restart. That part is often vague in real procedures. Review specifications with people who pack and inspect products; their feedback can expose confusing instructions. Still, too many checks can slow work and encourage rushed sign-offs, so test the process on the actual line and revise it when evidence shows a better approach.
Packaging accuracy depends on equipment that is set up correctly and checked often. Calibrate scales, fillers, label applicators, and inspection sensors against known standards. A small drift in a filling nozzle can create a steady run of underfilled or overfilled packages. Keep calibration records with dates, readings, and adjustments, so recurring changes are easier to spot. Check critical settings at the start of a shift and after a changeover. It takes time. But guessing takes longer.
A clean, well-maintained line also helps keep results consistent. Remove product residue from contact surfaces, inspect belts for wear, and check that guides hold packages straight. Loose fasteners or a worn conveyor can shift containers just enough to misalign labels. Follow a practical maintenance schedule, but leave room for condition-based checks; machines do not always wear at the same rate. Train operators to report unusual vibration, leaks, or repeated jams instead of simply restarting the line. Small warning signs matter.
Do not assume a successful calibration lasts indefinitely. Compare samples from the beginning, middle, and end of a production run, and investigate differences before they become routine. One weak point is hurried changeovers: teams may skip a check when production is behind. Set a clear verification step before the next batch starts, and record who completed it.
| No. | Improvement Area | Recommended Control | Suggested Check Frequency | Useful Measure |
|---|---|---|---|---|
| 1 | Calibrate filling and dosing equipment | Verify output against a traceable reference weight or volume. Adjust the set point when results drift, and record the before-and-after readings. | At startup, after product or format changes, and at a risk-based interval during production | Difference between the measured fill and the declared target |
| 2 | Check weighing scales and checkweighers | Use certified test weights that cover the working range. Confirm zero, span, and reject operation; keep reference weights clean and protected. | At startup and according to the site's documented calibration schedule | Test-weight error and correct reject rate during challenge checks |
| 3 | Maintain sealing equipment | Inspect sealing jaws, belts, heaters, and pressure settings. Confirm seal integrity using a method suitable for the package and product. | At startup, after adjustments, and during scheduled line inspections | Seal failures, leaks, or failed package-integrity tests |
| 4 | Verify temperature and pressure controls | Compare displayed readings with suitable calibrated instruments and check that operating settings remain within the validated process window. | At planned maintenance intervals and after repairs or control-system changes | Difference between the controller reading and reference reading |
| 5 | Inspect sensors and photoelectric eyes | Clean lenses, check mounting and alignment, and confirm reliable detection of containers, labels, and packaging material. | At line startup and during routine cleaning and inspection | Missed detections, false triggers, and sensor-related stoppages |
| 6 | Set up changeovers consistently | Use approved setup instructions for each product and pack format. Verify guides, tooling, recipes, and machine settings before restarting production. | At every product, material, or format change | First-pass acceptance rate after changeover |
| 7 | Standardize operator checks | Provide clear work instructions and record checks for fill, closure, label position, date code, and package condition. | At startup and at documented intervals during the run | Completion of required checks and number of defects found |
| 8 | Use preventive maintenance | Follow equipment maintenance plans for lubrication, wear-part replacement, cleaning, and inspection; document completed work and follow-up actions. | According to manufacturer guidance and maintenance history | Unplanned downtime and repeat equipment faults |
| 9 | Control packaging-material variation | Inspect incoming materials for relevant specifications such as dimensions, thickness, print registration, and sealability before use. | For each incoming lot, using a documented sampling plan | Material nonconformances and packaging defects by lot |
| 10 | Review process data and correct drift | Trend fill weights, reject counts, seal checks, and downtime. Investigate recurring patterns and document corrective actions. | During production review and at regular quality meetings | Process variation, defect rate, and recurrence of identified issues |
Note: Set acceptance limits, sampling frequencies, and calibration intervals according to product requirements, applicable regulations, equipment guidance, and a documented risk assessment.
Automating filling, labeling, and sealing can make packaging more consistent from one shift to the next. A filling system can dispense a set volume or weight, while sensors flag containers that fall outside the selected range. For example, a short fill detected before capping is easier to correct than a weak seal discovered during a later inspection. Keep containers aligned, too. A small guide adjustment can prevent labels from drifting across curved bottles.
Labeling equipment can check print placement and scan barcodes as packages move along the line. Set clear tolerances for label position, date codes, and legibility. Then record inspection results, so recurring errors can be traced to a specific machine setting or material batch. Small checks matter. A smudged code is easy to miss at speed.
Sealing automation helps control pressure, temperature, or dwell time, depending on the package and sealing method. Test settings with the actual packaging materials before routine production, and recheck them after changeovers. Automation still needs people. Operators should inspect samples, clean sensors, and respond to alarms instead of simply clearing them. One limitation is that sensors can drift or become obscured; even a well-tuned line may need adjustment after a material change. That is inconvenient, but ignoring it invites inconsistent packs.
Top 10 Ways to Improve Packaging Consistency and Accuracy
Inspect Materials and Verify Package Accuracy
Consistent packaging starts with checking materials before production begins. Examine cartons for crushed corners, uneven folds, and damp spots. Check labels for clear print, correct colors, and readable batch details. Small defects can become harder to spot once packages move quickly along the line.
Use a simple inspection checklist and compare each item with an approved sample. Verify package dimensions, seal placement, label position, and printed information. A ruler and a few marked reference points can reveal drift between shifts. Keep samples from different production runs, then review them side by side. This practical habit helps teams notice gradual changes, though human checks may still miss defects during busy periods. Do not treat one successful inspection as proof that every package is accurate.
Tips: Inspect materials under bright, even lighting. Check a small sample at the start of each shift and after setup changes. Record defects, even minor ones, and note where they appeared. If the same issue returns, pause and investigate the equipment or handling step rather than simply correcting each package by hand.
Inspect materials and verify package accuracy at key checkpoints. The values below are illustrative inspection rates, not results from a specific company or study.
Staff training is a practical control for packaging accuracy, not a one-time orientation. Teach operators to verify product codes, label position, fill levels, and seal condition at the machine. Use real examples: a crooked label, a faint date code, or a carton flap that will not stay closed. Keep instructions beside the line, where they can be checked during changeovers. Short refreshers help. The World Economic Forum’s Future of Jobs Report 2025 estimates that 39% of workers’ core skills will change by 2030, reinforcing the need for ongoing skills development.
Make training specific to each task and measure whether it works. Ask operators to demonstrate a changeover, then check their setup against a standard checklist. Track mislabeling, rejected packs, rework, and start-up waste by shift and product. Review the figures with the people doing the work; they may spot a recurring sensor fault or unclear instruction before a manager does. The Manufacturing Institute and Deloitte projected that 1.9 million U.S. manufacturing jobs could go unfilled by 2033, making practical knowledge-sharing especially important.
Keep records simple: note the date, task, trainer, and any follow-up needed. A line can meet its hourly target and still produce inconsistent packs. That deserves a closer look. Resist blaming operators too quickly; worn guides, rushed changeovers, and confusing work instructions can also drive errors. Regular observation matters, but it should support coaching, not just surveillance.
Record dimensions, materials, print position, closure type, and acceptable tolerances. “Looks about right” is not measurable.
Set clear checks for label placement, readable text, and secure seals. Keep approved samples beside the packing line.
Include examples of acceptable and unacceptable packs, such as a centered label and a visibly skewed one. Small details matter.
Check samples at the start of a shift, then repeat after material changes or machine adjustments. Ten packs can provide a simple starting check.
Record skewed labels, crushed corners, inconsistent fills, and other visible issues. Assign clear actions for each failure.
Filling systems can dispense set volumes or weights and flag containers outside the selected range. Catching a short fill before capping is easier.
Check label position, date-code legibility, and barcode readability. Record results to help trace recurring errors to settings or material batches.
Pressure, temperature, and dwell time may need adjustment after a changeover. Sensors can drift or become obscured. People still matter.
Ask packing and inspection staff to review instructions, then test them on the actual line. Too many checks may encourage rushed sign-offs, so the process deserves another look.
Improving packaging consistency and accuracy starts with clear, documented specifications and quality standards. Define requirements for package dimensions, fill levels, labeling, sealing, and acceptable tolerances so that every production run has measurable targets. Regularly calibrate equipment and maintain packaging lines to reduce variation, prevent avoidable errors, and keep machinery operating reliably. Automation can further support repeatable filling, labeling, and sealing by reducing manual handling and helping processes stay consistent at different production speeds.
A practical approach to how to improve packaging consistency and accuracy also includes inspecting incoming materials and verifying finished packages throughout production. Check that packaging materials meet specifications, and use suitable measurements or visual checks to confirm quantities, labels, and seals. Train staff to follow standard procedures, recognize defects, and report issues promptly. Finally, monitor production performance and review inspection results over time. Using this information to adjust processes helps teams catch recurring problems early and steadily improve packaging quality.
Nexa Machine